A sample can have the right feel, color, and fit, yet leave a buyer uncertain about the order that follows. Tiles from different cartons need to connect properly, and a repeat order may need to match stock already on the shelf. If part of a delivery feels softer, the supplier needs a way to identify the affected production run.
Foam mat batch consistency means keeping the product’s key characteristics within agreed limits across a production run and subsequent orders. It requires an approved specification, comparable measurements, and records that connect finished mats to their materials and processing history.
The evidence should let you compare production groups, see where a change started, and understand what happened to the affected stock.
Define what must stay consistent
Perfectly identical measurements are an unrealistic purchasing requirement. A useful specification describes the variation the product can tolerate while still meeting its intended use, appearance, and assembly requirements.
For interlocking mats, tooth fit and assembled dimensions may matter as much as a single tile’s size. A printed play mat needs consistent graphic placement and surface condition. A yoga mat program may place greater weight on thickness, surface feel and flat lay after unpacking.
Choose the characteristics that affect the customer’s experience, then assign a target or reference, an acceptance rule and a comparison method. Keep density, hardness and thickness as separate entries when all three matter; one result cannot stand in for the others.
| Product concern | Requirement to carry into production | Useful record |
|---|---|---|
| Mats feel different between cartons | Named hardness or compression method, specimen arrangement and acceptance limits | Individual readings linked to production groups |
| Tiles do not fit consistently | Drawing revision, tooth profile, dimensions and assembly check | Tool identification and representative assembled-set results |
| Colors differ on a retail display | Approved color reference and agreed viewing or instrumental method | Results identified by color, material lot and surface construction |
| Printed or laminated faces vary | Artwork revision, registration, texture and relevant adhesion or wear requirements | Surface-processing run and finished-sample checks |
| Mats arrive curled or compressed | Agreed pack format and unpacking/conditioning procedure | Packaging revision and evaluation at a stated interval |
The foam mat sample approval checklist helps establish that initial reference. Once approved, production reproduces the defined requirements and records changes that could affect them.
What counts as a batch?
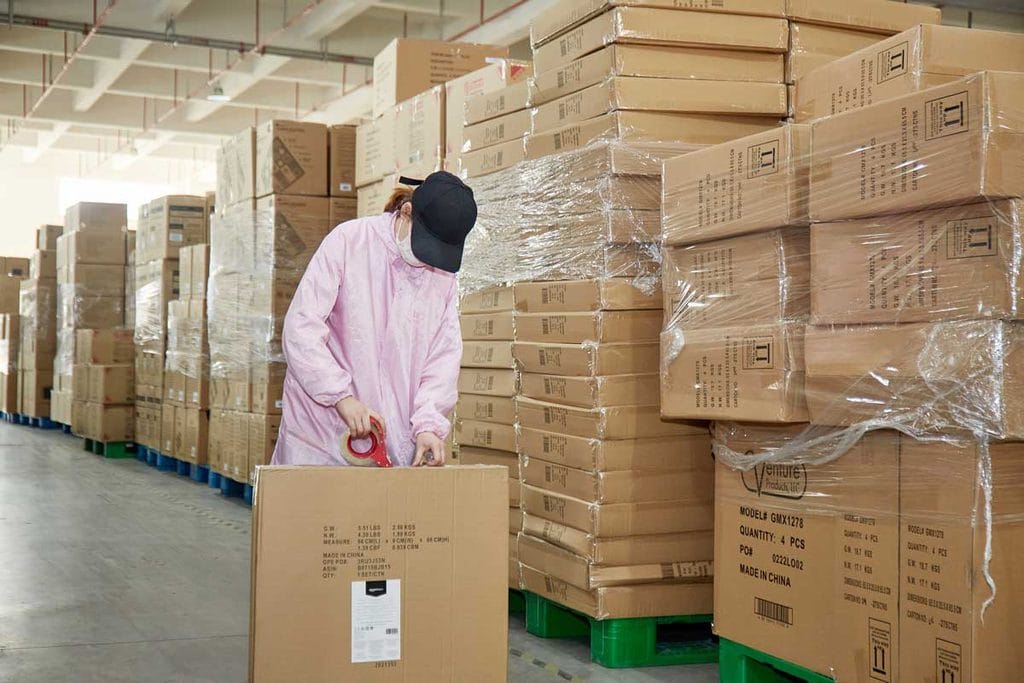
A purchase order, a mixing batch, and a shipment are different groupings. One order may contain several compound mixes, foaming runs, cutting operations, and printing runs. A carton can even contain pieces from more than one production group unless packing rules keep them separate.
The supplier’s lot structure should connect the finished product to its history:
Raw-material lots → compound batch → foam sheet, block or roll → converting and surface-processing run → finished lot → cartons or pallets.
The exact labels depend on the factory. What matters is whether the connections survive when material is split, combined, moved to another operation, or reworked. If two foam batches enter one finished lot, preserve both parent references. If a suspect roll feeds several cutting runs, the record should identify all affected finished goods.
The code the buyer sees must lead back to those records. A carton code loses much of its value if repacking removes the only connection to the production lot. Mixed assortments and replacement-tile programs therefore need an agreed way to retain identification through the relevant packing and distribution steps.
Why an unchanged product name can produce a different mat
Material identity and formulation revision
“EVA foam” does not identify a complete formulation. Resin grade, blend components, additives, pigment, and any approved recovered material are part of the production specification. A substitution can preserve the broad material name while changing the processing behavior or finished result.
In an EVA system using azodicarbonamide (AC) for blowing and dicumyl peroxide (DCP) for crosslinking, gas generation and network formation interact with the molding conditions. Changes in additive dosage or the heating cycle can alter expansion and final properties. Workable settings depend on the formulation, so a supplier must control the approved combination rather than copy a recipe from another product. [1]
Identify the approved formulation revision and agree on substitution rules. A buyer does not necessarily need the supplier’s confidential recipe. The supplier can retain the detailed formulation while providing controlled revision IDs, material-lot records, and notification of agreed significant changes.
Records from compounding and mixing connect weighed inputs and additions to the compound used in an order. That connection helps the supplier investigate a difference without relying on the finished mat’s appearance to guess what changed.
Processing and finishing history
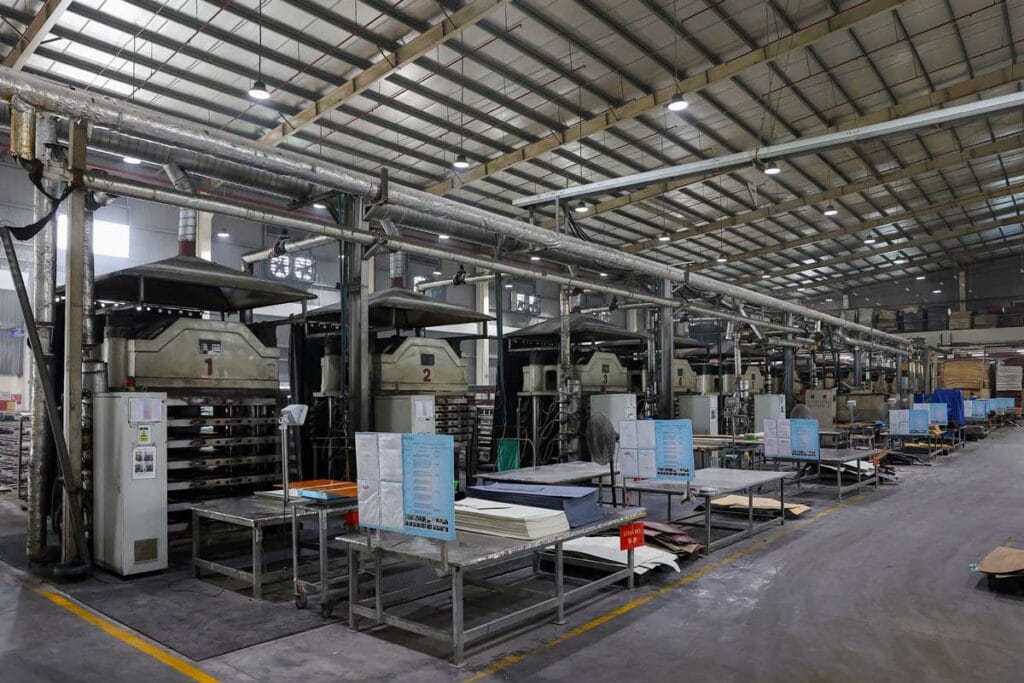
The same formulation still needs a controlled manufacturing route. Mixing, foaming, cooling, cutting, and surface processing each contribute to the finished product. Useful run records capture the conditions relevant to the characteristic being checked, along with equipment or tool identity.
A setup sheet describes what was intended; run records show what was recorded during production. For temperature control, for example, a heater setpoint and a measured process temperature are different entries. Their meaning depends on the sensor and measurement location.
Changes downstream can matter even when the foam core is unchanged. A different cutting tool can affect fit; a revised film or ink can alter the finished face; a tighter pack can change the condition in which the customer first evaluates the mat. Preserve the connection between these operations and the finished lot.
Confirm the measurements before judging the batch
Suppose the buyer measures a mat immediately after unpacking, while the factory measured its reference after an agreed conditioning period. A difference between those readings does not yet establish a production change. The specimens need comparable preparation before the results can resolve the question.
A thickness reading taken at an embossed peak is not directly comparable with one taken in a valley. A hardness result needs its scale, specimen support, thickness, and reading procedure. A density result needs a stated basis, particularly if one specimen includes a surface layer that the other excludes.
Shared measurement instructions make the comparison repeatable: both parties use the same specimen arrangement, locations, conditioning, instrument requirements,, and reporting units. When a dispute remains, matched specimens help isolate the source of disagreement. Destructive tests require an agreed way to select comparable specimens because you can’t always test the same piece twice.
Calibration supports confidence in the instrument, while the working procedure must also produce consistent results across operators. Resolution, contact pressure and specimen positioning become especially relevant near an acceptance limit. ISO 10012 covers the entire measurement process; product tolerances still need to be agreed for the mat.
The guide to reading a foam mat test report explains each metric. For batch control, the method must remain comparable over time, and any method change must be recorded.
Sample across the run, not only from the submitted carton
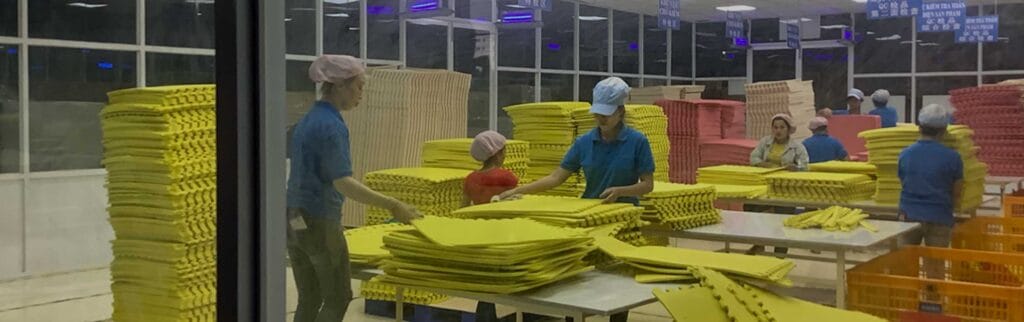
Several readings from one small piece reveal little about variation across an order. The sampling plan should reflect how the mats are made and where a change could appear.
For a sheet or roll process, consider position across the width and progress through the run. For molded products, preserve mold or cavity identity where relevant. Include different compound batches when one order spans them. New material lots, restarts, and significant setup changes can justify additional checks.
Define sample numbers and frequency with the supplier according to order size, production history, product risk, and the variability being investigated. For each check, name the responsible person, the point in production, and the action required when a result fails or signals a change. State who can release held material after review.
Individual results need sample IDs and their place in the production sequence. This separates variation within one run from differences between runs.
For example, in a hypothetical puzzle-mat order, tiles from two cutting runs might each pass an individual dimension check but fit poorly when mixed. The control plan should include the relevant combination of tiles, not only measurements of isolated pieces. The dimensional stability guide explains the geometry and conditioning questions behind that comparison.
How to compare batch results
Start with the individual readings before looking at the batch average. An average can hide pieces at opposite ends of a tolerance band or mask a shift when early and late production are combined.
Read the results in this order:
- Check comparability. Confirm the product revision, measurement method, specimen preparation, and units. Separate groups that cannot reasonably be compared.
- Check individual results against the specification. Identify failures and borderline readings that need review under the agreed decision rule. A passing average does not cancel an individual failure where the requirement applies to each unit.
- Look within each batch. Examine the spread and the locations of unusual readings. A pattern across a sheet or a difference between cavities gives the investigation a more useful starting point than a single order-wide average.
- Compare batches and production time. Look for shifts in the typical result, changes in spread, and differences following restarts or substitutions. Preserve the group identities so that combining data does not conceal a change.
For example, two batches could have similar average thickness but different variation: one tightly grouped, the other containing more pieces near either limit. Whether both are acceptable depends on the specification and results, but the wider spread warrants attention when planning future production.
When every reading passes but the process is shifting
Thickness might remain within specification while successive readings move toward one limit. The latest pass result alone will not show that pattern. Time-ordered data help reveal whether the process continues to behave consistently, as explained in NIST’s process-stability guidance.
The buyer’s specification limits define the product requirement. Statistical control limits help flag changes in process behavior. A signal calls for investigation; it does not replace the product’s acceptance rule. Conversely, a predictable process can still produce outside the required range. NIST’s control-chart guidance explains this distinction.
Some suppliers summarize performance with a process capability index such as Cpk. Interpret it only with the characteristic, production period, sampling basis, and data assumptions behind it. Capability evaluation depends on a stable process and suitable data; pooling data from different products or operating conditions can make a headline figure misleading.
For a short custom run, a clear measurement log and a documented response to deviations may be more useful than a capability number that the available data cannot support.
Keep color and assembly comparisons tied to the reference
A repeat order may sit beside earlier stock. That makes cross-order comparison a commercial requirement, even when each order appears acceptable on its own.
For color, retain the approved master and identify its storage conditions. Use the agreed lighting, orientation, and viewing arrangement. Include texture, gloss, and surface layers in the comparison. If instrumental color difference is specified, name the calculation method and measurement setup as well as the limit.
Avoid letting each shipment become the unrecorded reference for the next. Small successive changes can move the product away from the original approval. Replacing an aged reference should be a documented decision, with the new reference linked to the specification and approval history.
For interlocking products, decide whether new tiles must fit earlier production. If replacement compatibility is part of the offer, assess new production against a controlled earlier reference as well as against itself. Where designs or tools have changed, make compatibility and labeling decisions explicit before mixing stock.
Before placing a repeat order
“Same as last order” is useful only when both parties know which specification and production record it refers to. Compare the proposed run with the last approved construction, including any temporary concession. An exception accepted for one delivery should not quietly become the normal specification.
A long gap can introduce practical changes: the original resin grade may be unavailable, a tool may have been replaced, or the retained sample may have aged. Evaluate a proposed substitute against the properties it could affect. Matching the material name or color alone is insufficient evidence of equivalence.
The repeat-order review should answer three questions: what has changed, what evidence supports the change, and which lot will introduce it? Where old and new inventory may be sold or installed together, include appearance and assembly compatibility in that decision.
The purchasing agreement should identify which changes require buyer approval and who can authorize release. The supplier can then manage routine adjustments within the approved process range while escalating changes that affect the agreed product definition.
What to do when bulk mats differ from the sample
First, identify the extent of the problem while preserving evidence.
- Identify and hold the suspect material. Record the finished-lot and carton IDs, the affected quantity, and the stock location. Prevent unreviewed mixing or release while you assess the issue.
- Confirm the comparison. Check the approved revision, sample condition, measurement method, and units. Keep the original failed results and photographs.
- Trace the production window. Compare affected and unaffected material with their raw-material, processing, and finishing records. Establish the last confirmed acceptable point and the next verified acceptable point where records allow it.
- Agree on disposition. Document whether goods will be sorted, reworked, rejected, or accepted under a specific authorized concession. Define the scope of any concession rather than treating it as a permanent specification change.
- Verify the correction. Review identified output after the action and monitor the next relevant production interval or lot. A corrected sample alone provides little evidence that you have controlled the cause.
The common foam mat quality defects guide can help describe the symptom. Use production evidence to investigate the cause: appearance alone cannot establish that a formulation, machine, or operator caused the difference.
If sorting or rework takes place, preserve the original lot relationship and identify the resulting accepted stock. The buyer should be able to distinguish the original production result from the result after intervention.
Request a compact batch record
The record should let both parties reconstruct what was produced, how it was checked, and who authorized its release. It can remain concise.
| Record group | Information to agree |
|---|---|
| Product reference | SKU, specification revision, approved sample ID, artwork and pack revisions |
| Material history | Relevant input lot IDs, formulation revision and authorized substitutions |
| Production history | Compound and foam-run IDs, relevant equipment/tool references, dates and significant changes |
| Measurements | Sample IDs and locations, method, conditioning, individual results and acceptance limits |
| Exceptions | Failed checks, containment, rework, concessions and follow-up results |
| Shipment mapping | Finished-lot IDs linked to cartons or pallets and shipment reference |
| Retention | Samples or representative pieces kept, storage conditions, retention period and record access |
A certificate of analysis is useful only for the lot and properties it actually describes. Ask whether the values come from that lot’s testing or from typical material data. A resin supplier’s certificate does not, by itself, establish the dimensions or performance of the converted mat.
Batch records support the wider foam mat quality-control plan. Final inspection remains a separate release activity. If an AQL-based scheme is agreed, ISO 2859-1 provides lot-by-lot acceptance-sampling schemes; passing an inspection sample does not show every unit is identical or establish process capability.
Questions buyers ask about batch consistency
No. Compare the other specified characteristics, such as hardness, thickness, recovery, surface condition, and fit. Density is one part of the product definition, and its measurement basis must also match.
The control plan should distinguish routine production checks from periodic and change-triggered testing. Set the frequency according to the property, product requirements, applicable obligations, and production history. Record which tests support the lot being supplied and which establish a broader qualification.
Only when the agreed packing and traceability requirements allow it and the relevant product checks support mixing. Consider appearance within the set, assembly compatibility, and the ability to identify affected stock later. A common SKU alone does not establish that two batches are suitable for the same pack.
Confirm the SKU and revision, then compare conditioning, packaging history, and the measurement procedure. If the difference remains, use the lot records to examine changes in inputs and production. Keep an untouched representative sample from the affected shipment for the investigation.
Discuss Your Repeat-Order Requirements
Send NEEU the approved specification, sample reference, and the characteristics that need to remain consistent across deliveries. For an existing mismatch, include the affected lot IDs, measured differences, and comparison conditions. These details provide a starting point for reviewing the production records and agreeing on the evidence required for the next order.
References
- Feng Shaohua, Liu Zhongjie, Zuo Jiandong, Zeng Jianguo and Hao Jiandong.[EVA Crosslinking Foaming Technology and Applications]. Plastics Science and Technology, 2003, issue 2, pp. 9-11, continued p. 15. ↩︎
- ISO. ISO 10012:2026: Quality management – Requirements for measurement management systems.
- NIST/SEMATECH e-Handbook of Statistical Methods. Assessing Process Stability.
- NIST/SEMATECH e-Handbook of Statistical Methods. What are Variables Control Charts?.
- NIST/SEMATECH e-Handbook of Statistical Methods. What is Process Capability?.
- ISO. ISO 2859-1:2026: Sampling procedures for inspection by attributes – Part 1.